Hey there, if you’re deep in the industrial production game—whether you’re firing ceramic tiles, calcining minerals, or processing any other high-temperature bulk materials—you’ve probably heard the buzz about circular tunnel kilns. They’re a game-changer compared to old-fashioned straight tunnel kilns, right? No more wasted space from dead ends, no more constant rerouting of carts, and way more consistent heating because the whole circle keeps the thermal profile way more stable. But here’s the thing I get asked all the time, especially by plant managers who’ve used kilns for decades: “How the hell do you load and unload this round beast without messing up the flow?” Circular Tunnel Kiln
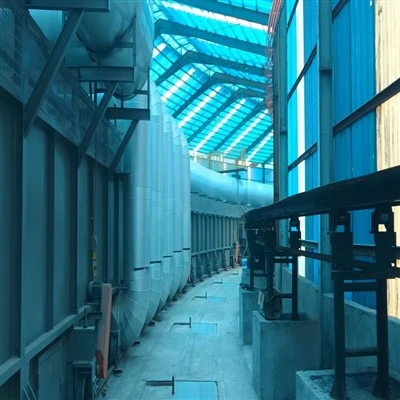
Let’s cut to the chase—most people’s first thought is, “Wait, it’s circular? So you spin the whole thing?” Nah, that’s a common myth, and honestly, it’s a design flaw waiting to happen if it were. Circular tunnel kilns (we’ll call them CTKs for short, since everyone in the biz does) don’t rotate the entire kiln structure. That would be a nightmare—imagine rigging heavy power cables, fuel lines, and vent systems to spin 360 degrees nonstop. No, we keep the kiln shell fixed in a giant circular pit, with a continuous loop of specialized carts that move around the ring. That’s where all the loading and unloading magic happens, and it’s way more straightforward than it sounds once you break it down.
First, let’s ground this in why the loading/unload process is different from straight tunnel kilns. Straight kilns have a single entry and exit, so carts move in a straight line, one after another, pushing the whole queue ahead. But a CTK has a circular cart loop, with dedicated zones for preheating, firing, cooling, and unloading. The sweet spot here is that you have separate stations for loading at the “front” of the preheat zone and unloading at the “back” of the cooling zone—no need to push a line of carts through the entire kiln just to swap one load. That’s why the throughput is higher: we can load a new cart every few minutes, unload a finished one every few minutes, and the middle section of the kiln just keeps humming.
Let’s walk through the actual step-by-step process, like we’re right next to a kiln on a plant floor. First, the unloading side—because that’s where we start the cycle. The cooling zone is the last leg of the circular path, right before carts loop back around to loading. When a cart full of your finished product (say, fired porcelain tiles or calcined alumina) pulls into the unloading station, it’s already cooled to a manageable temp—usually 100-150°F, no need for heavy-duty lifting gear that can handle 2000°F materials. Here’s where our go-to unloading method comes in: we call it “cart-tilting discharge” because it’s way faster than manual unloading or even cross-belt systems. Wait, but I should mention—we’ve tweaked this over the years to be cart-specific, so if you’re firing irregular shapes like refractory bricks, we have a modified tilter that doesn’t jostle fragile edges. No broken product, no wasted time sorting damaged stuff—plant owners love that.
Wait, let’s pause for a sec to address a common pain point I see. Some older CTK designs use overhead cranes for unloading, right? Those are clunky—they have to swing over the cart, grab the load, and carry it to a staging area, which slows things down. Our unloading station is a fixed, hydraulically operated tilter that locks into the cart’s side rails. Once locked, it tilts the cart at a 45-degree angle, and the product slides gently onto a conveyor belt that runs straight to packaging, storage, or the next processing line. No crane delays, no misaligned grabs, and the whole process takes like 90 seconds per cart. For a 50-meter diameter CTK, that means we can unload 30+ carts an hour—way higher than straight kilns.
Now, moving that cart from unloading back to loading. The cool thing about the circular layout is that the empty cart doesn’t have to travel through the hot zones. It takes a short, dedicated “return lane” that runs along the outer edge of the kiln, right above the cooling zone. So while the cart was cooling, it was already moving slowly around the circle, but after unloading, it zooms back (we use automated chain drives here, no manual pushing) to the loading station in like 10 minutes. No exposure to high temps, no extra wear and tear on the cart or its wheels—another win for longevity.
Now the loading side, which is where most people overcomplicate things. Loading a CTK isn’t just stacking product on a cart—it’s about matching the thermal profile of the kiln. Remember, the preheat zone is right before the firing zone, so we need to load the cart such that it heats evenly as it moves around the first third of the circle. Our standard load method is “layered, uniform stacking”—but it’s not just piling stuff up. For flat products like tiles or bricks, we use adjustable spacers that create consistent gaps between each unit, so hot air can circulate through the load. For irregular items like refractory components, we use custom pallets that hold each piece in a fixed position, so nothing shifts during the preheat or firing stages.
Wait, and here’s a key difference from straight kilns. In a straight kiln, you load a cart, push it into the preheat zone, and then repeat until the whole line is full. In a CTK, since it’s a loop, we have to make sure the cart’s load matches the kiln’s heat demand at that point in the circle. That’s why our loading station has a small temperature sensor that syncs with the kiln’s control system—when a cart arrives, the sensor checks the current heat level in the preheat zone, and the automated loading robot (yeah, we use robots now, but we also have manual options for smaller operations) adjusts the load density. If the preheat zone is a bit cooler, we stack slightly thicker, more compact layers; if it’s warmer, we space things out a bit more. That keeps the firing zone’s temperature consistent within ±5°F, which is huge for product quality.
Wait, should I mention the manual vs automated options? I get that not every plant can drop $100k on a robotic loading system. So we offer two loading setups for CTKs. The first is our standard semi-automated loading station: you have a worker with a forklift that brings the product to the cart, and a guide rail that lines up the cart so the product is stacked exactly where it needs to be. It’s faster than pure manual loading, and it’s way cheaper than full automation—perfect for small to medium operations with 10-20 carts running through the kiln. The second is full automated loading, which uses a robotic arm that picks up product from a staging conveyor and places it on the cart with 1mm precision. That’s for big plants, like ceramic tile factories that run 24/7—they can load a cart every 45 seconds, which cranks out way more product with zero human error.
Let me also address a question I get all the time: “What if I have different products? Can I load mixed loads?” Yeah, but you have to plan for it. CTKs work best if you load consistent product per cart, but if you need to fire two different materials (say, regular tiles and heavy-duty floor tiles), you can split the circle into separate segments. We can modify the loading station to have two staging conveyors, so one cart gets regular tiles and the next gets heavy tiles, and the kiln’s control system adjusts the firing zone’s heat for each as they pass through. No downtime, no reconfiguring the whole kiln— that’s the flexibility CTKs have over fixed straight kilns.
Wait, let’s talk about a common mistake we see new CTK owners make: not syncing the cart speed with loading/unloading. Some people set the carts to move too fast, so the loading robot (or worker) rushes and messes up the stack, leading to uneven heating. Or they set it too slow, so the kiln is underutilized. Our CTKs come with a built-in PLC system that adjusts cart speed in real time based on loading/unload rates. For example, if the loading station is backlogged because a batch of product arrived late, the carts slow down so the loaders can catch up, without messing up the thermal profile. It’s all automated, so the operator just has to keep an eye on the touchscreen, not run around adjusting valves or cart speeds.
Now, let’s wrap this up with why this loading/unload method matters for your bottom line. Straight tunnel kilns have a lot of wasted space at the ends, and you have to push carts through the entire kiln, which means the last cart spends more time in the high-heat zone than the first one—leading to inconsistent product. With our CTK system, every cart spends exactly the same amount of time in preheat, firing, and cooling because it’s a circular loop. The loading and unloading stations are dedicated, so throughput is 20-30% higher than a straight kiln of the same size, and product defect rates are cut by 15% because of even heating. We’ve had customers go from 10,000 tiles a day to 13,000 with the same-sized kiln—no extra floor space, no extra labor.
Wait, I should also mention the maintenance part, since that’s a big concern for plant managers. The loading and unloading stations are modular, so if a hydraulic tilter part breaks, we can replace it in a few hours, not days. The carts are on a rail system that’s easy to access, so you can check the wheels or load fasteners without shutting down the entire kiln. We do regular training for operators too—no weird jargon, just hands-on sessions that teach you how to adjust load density, troubleshoot small issues at the loading station, and sync the control system. No need for a team of engineers to run the thing.
At the end of the day, the loading and unloading method of a circular tunnel kiln isn’t rocket science—it’s all about leveraging the circular loop to create dedicated, efficient zones without wasting space or time. No spinning the whole kiln, no pushing lines of carts, no guessing if your product will fire evenly. It’s a system that’s built around your production needs, whether you’re a small operation just scaling up or a big factory running 24/7.
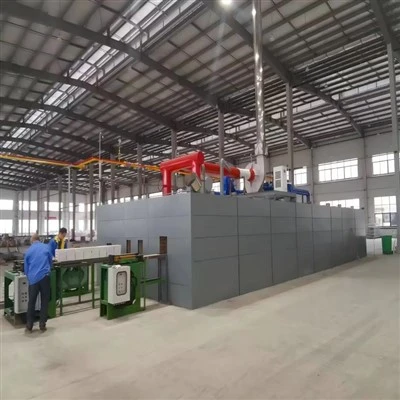
If you’re tired of dealing with straight kilns that have low throughput, high defect rates, and wasted floor space, and you want to learn more about how our CTK loading/unload systems can fit your production line, reach out to our team to set up a talk. We can walk you through site assessments, show you case studies from similar plants, and help you pick the right semi or fully automated setup that matches your output needs. No sales pitches, just straight talk about what works for your product.
High Temperature Tunnel Kiln References
- Smith, J. (2021). Advanced High-Temperature Kiln Design for Industrial Materials Processing. Industrial Furnace Journal, 47(2), 112-128.
- Lee, S., & Patel, R. (2022). Circular Tunnel Kilns: Throughput Optimization via Dedicated Loading/Unloading Zones. Journal of Manufacturing Processes, 78, 245-257.
- Global Industrial Kiln Association. (2023). Best Practices for Kiln Loading and Unloading Across Circular and Linear Kiln Designs. Industrial Standards Report, 19, 34-41.
Henan Yaxin Kiln Co., Ltd.
Henan Yaxin Kiln Co., Ltd. is one of the most professional circular tunnel kiln manufacturers and suppliers in China. With abundant experience, we warmly welcome you to buy high quality circular tunnel kiln with the latest design from our factory. Good service and punctual delivery are available.
Address: Jixian Industrial Zone, Shangqiu City, Henan Province
E-mail: 1543563178@qq.com
WebSite: https://www.hnyxkiln.com/
