Hey there, if you’ve ever hung around a steel mill floor, you’ve probably seen that massive, rumbling steel billet reheating furnace chugging along like a grumpy but essential old beast—blowing heat like it’s got a point to prove, turning cold, solid steel blocks into squishy, malleable blanks ready for rolling or forging. And if you’ve ever asked someone who actually works with these things, “Wait, how hot does that thing get, anyway?” you might’ve gotten a shrug, a mumble about “it depends”, or a vague number that doesn’t do the job. As a steel billet reheating furnace supplier who’s spent the last 12 years troubleshooting, tweaking, and fine-tuning these bad boys for mills big and small across North America and beyond, let me cut through the noise and lay it all out straight—no jargon, no fluff, just what you actually need to know about their temperature control range. Steel Billet Reheating Furnace
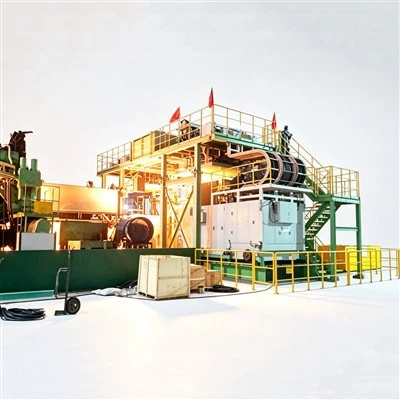
First off, let’s get one thing out of the way: there’s no one-size-fits-all number here. A billet reheating furnace isn’t a toaster where you set 350°F and walk away—your average toaster is tiny, heats one slice, and doesn’t have to account for 5,000-pound steel blocks that might be 3 feet long and a foot wide. Billet furnaces are built for specific jobs, and that job is the single biggest driver of their temp range. Let’s break down the main use cases first, because that’s where everything starts.
If your mill’s running short, small billets—say, 3-inch round blocks for rebar or wire rod—they don’t need to get screaming hot. Those might go through what we call a “low-temp” reheat cycle, where the furnace’s operating band is roughly 1,100°C to 1,250°C (that’s 2,010°F to 2,280°F, for all you imperial folks). Why not hotter here? Because rebar doesn’t need super high plasticity—just enough to bend it through rolling stands without cracking, and going any hotter wastes fuel (which mill operators care about, trust me). On the flip end, if you’re forging heavy equipment parts—like gear blanks for mining trucks, or massive axle shafts for railcars—those 10-inch thick billets need way more heat to get all the way through, right down to their core. That’s where we’re talking 1,250°C to 1,350°C (2,280°F to 2,460°F) minimum, and some custom furnaces we’ve built for heavy forging even nudge up to 1,400°C (2,550°F) for super thick, high-alloy billets.
But wait—this is just the max and min operating temps. The real magic is in the temperature control range—that sweet, narrow window the furnace has to hit every single billet, no matter where it is on the conveyor. Let’s be real: if you put a cold billet into a furnace, the part closest to the burners is gonna heat up faster than the part in the middle, and the billet’s far end might be a little cooler. A good furnace doesn’t just blast heat randomly to make up for that—its control system is built to hold a uniform temp across every zone, and that’s where the control range matters. Most modern billet reheating furnaces (the ones we sell, at least) split the heating chamber into 3 to 5 separate zones: preheat, heat, and soak. The preheat zone is where the cold billet starts, so it’s a little cooler (800°C to 1,000°C, 1,470°F to 1,830°F) to prevent thermal shock—you don’t wanna toss a solid cold block into 1,300°C heat and crack it like a ice cube. Then the heat zone ramps up to that high temp we talked about, and the soak zone holds it steady for 10 to 15 minutes to make sure the core matches the surface.
Here’s the part most people get wrong: the control accuracy is way more important than the raw max temp. Let’s say two furnaces both have a top temp of 1,350°C. One might hold that within ±10°C (±18°F) across the whole chamber, the other might swing ±50°C (±90°F) like a faulty thermostat. What does that mean for you? If your billet’s temp is 50°C lower than it needs to, it’ll crack during rolling, and you’ve got a $5,000 billet waste. If it’s 50°C higher, you’re wasting fuel, and the steel’s grain structure gets messed up—your finished parts will be weaker than they’re supposed to. So as a supplier, we don’t brag about our max temp—we brag about our control system that holds that 20°C window like glue.
Now, let’s talk about the exceptions, because there are always edge cases. What if you’re working with alloy steels—like stainless, tool steel, or high-carbon steel? Those bad boys are way more sensitive to temp than regular carbon steel. For example, tool steel needs to be at exactly 1,280°C (2,335°F) to get the right hardness when forged—go 20°C over, and it starts to oxidize (that’s the scaly gunk you have to grind off later, wasting time and material). For those, we build furnaces with tighter control ranges—sometimes ±5°C (±9°F) across all zones, and we even add oxygen monitoring to make sure we don’t get any unwanted reactions. On the flip side, some small, job shops that run a mix of billets might go with a slightly wider range, like 1,000°C to 1,300°C (1,830°F to 2,370°F), but only if they’re okay with a little more scaling and occasional scrap.
You might be wondering: why does this control range even matter to you, the person buying billets or running a mill? Let’s do the math. A mid-sized mill runs 200 billets a day, each 5,000 pounds. If your furnace’s control is off by 30°C, that’s 2% scrap per billet—100 pounds per billet, 20,000 pounds a day, that’s $20,000 a month in wasted steel, plus fuel wasted heating too-hot billets. That’s why when we talk about temperature control range, we’re not just talking numbers on a screen—we’re talking your bottom line, your downtime, and the quality of every part you ship.
I’ve seen plenty of mills go cheap on a used furnace or a cut-rate system, and guess what? They end up calling us 6 months later, complaining about scrap rates spiking and fuel bills through the roof. Last year, a guy from a mill in Ohio hit me up—they had a 10-year-old furnace that could only hold temps within ±40°C, and they were throwing out 12 billets a week. We retrofitted their control system, re-calibrated the burners, and got their accuracy down to ±12°C. His scrap rate dropped 80% in 30 days, and he saved over $15,000 a month on fuel. That’s the real value of getting this right.
So, to wrap this up quick, here’s the breakdown you can take with you: most standard carbon steel billet reheating furnaces have a total temperature range of about 800°C to 1,400°C (1,470°F to 2,550°F), but the control range (the accuracy they hold that temp) is what separates a good furnace from a bad one. For regular rebar or wire rod, you’ll operate in 1,100°C to 1,250°C with ±15°C control. For heavy forging, 1,250°C to 1,350°C with ±10°C. For alloy steels, narrower still, down to ±5°C. Always ask a supplier what their control accuracy is, not just their max temp—numbers look good, but results matter.
If you’re tired of scrap billets eating into your profits, or your fuel bills making your CFO grind their teeth, hit us up to chat. We don’t do hard sells—we listen to what you’re making, what your output needs are, and build or tweak a furnace that fits your exact needs, not some generic spec sheet. Whether you’re a small job shop running 50 billets a day or a massive mill cranking out 10,000, we’ve got you. Don’t guess at your furnace’s temp or waste money on subpar equipment—let’s talk about what’ll work for you.
Induction Quenching and Tempering Production Line References:
- ASM International. (2019). Heat Treater’s Guide: Practices and Procedures for Irons and Steels. ASM International.
- Steel Industry Energy Conservation Association. (2021). Reheating Furnace Efficiency and Temperature Control Best Practices. SIECA Technical Report.
- American Iron and Steel Institute. (2020). Billet Processing and Reheating Furnace Design Standards. AISI Publication 12-20.
Hebei Yuantuo Electromechanical Equipment Manufacturing Co., Ltd.
As one of the most professional manufacturers and suppliers of steel billet reheating furnace in China, our products have good reputation in the market. Please rest assured to buy advanced equipment made in China here and get quotation from our factory. Customized orders are welcome.
Address: Yanshan Street West and Jialingjiang Road North, Economic and Technological Development Zone, Wuqiao County, Cangzhou City, Hebei Province, China
E-mail: yuantuotech01@gmail.com
WebSite: https://www.yuantuoem.com/
